 inglés
 francés
 español
 ruso
 coreano
 Japonés japonés


Water-Soluble Microencapsulated Quercetin Powder 20% (Food Grade)
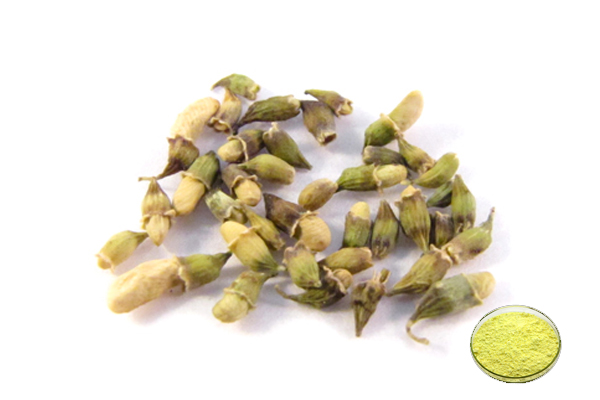
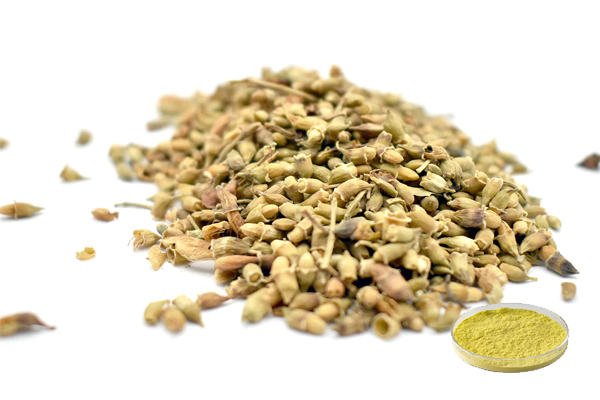
BotanicalSource:SophorajaponicaL. (Dried flowers and buds)
Active Ingredients: quercetina (Standardized Microencapsulated Form)
Assay : ≥20.0% Quercetin
Carrier: Food-Grade Maltodextrin / Arabic Gum Options
Método de ensayo: HPLC
Solubility & Dispersibility: Cold-Water Soluble (Forms a stable, homogeneous, and sediment-free solution)
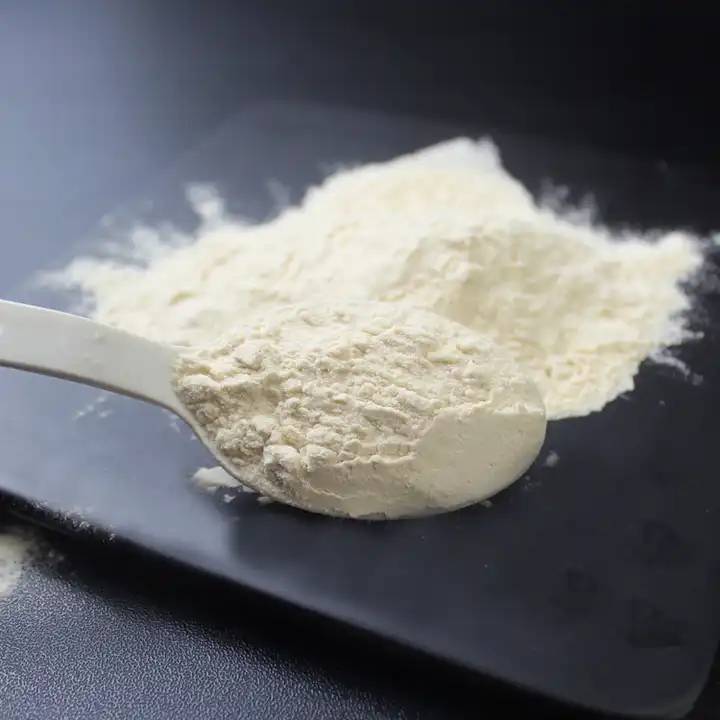
Aspecto: Light yellow to yellow fine powder
Regulatory Standards: Complies with USP <731>, USP <233>, EP 2.2.32, and (EC) No 396/2005
Certificates: BRCGS, IFS, COSMOS, Halal, Kosher, Organic (USDA/EU)
Sample: 10-50g Free Sample Available for R&D
- descripción
- Hoja de datos
-
What is Water-Soluble Quercetin Powder?
Water-Soluble Microencapsulated Quercetin Powder 20% is a food-grade, standardized botanical bioflavonoid preparation derived from the dried flowers and buds of Sophora japonica L. Utilizing an advanced spray-drying microencapsulation technology, the native hydrophobic quercetin molecule is embedded within a protective, hydrophilic food-grade carrier matrix. This physical modification standardizes the active quercetin content to ≥20.0% via HPLC, optimizing cold-water dispersibility for functional food and beverage manufacturing.
This highly dispersible clean-label powder dissolves rapidly in liquid matrices without generating visible cloudiness, localized precipitation, or gritty heavy sediment across wide industrial pH ranges. The specialized microencapsulation shell effectively masks the natural bitterness inherent to plant polyphenols, allowing for smooth sensory profiles without altering the primary flavor characteristics of the final delivery system. Additionally, the cross-linked protective carrier network prevents premature thermal oxidation or localized degradation during high-temperature commercial pasteurization processing.
The refined material matrix serves as a stable technical constituent for extending shelf-life uniformity and maintaining active consistency in complex formulations. This food-grade ingredient is engineered specifically for uniform dry blending and stable liquid dispersion, making it a reliable industrial solution for clean-label functional beverages, clear liquid supplements, instant powder stick packs, and dry-mix nutritional formulas.
especificación
Nombre del producto
Water-Soluble Microencapsulated Quercetin Powder
Nombre latino
Sophora japonica L.
CAS No.
117-39-5
Plant Part Used
Dried flowers and buds
Principios activos
Quercetin (Standardized Microencapsulated Form)
Carrier Food-Grade Maltodextrin / Arabic Gum Options Assay (On Anhydrous Basis) ≥20.0%
Método de ensayo
HPLC
apariencia
Light yellow to yellow fine powder
Particle Size 100% through 80 mesh Solubility & Dispersibility Cold-water dispersible (Forms a stable homogeneous dispersion) Clarity of Solution (1% Water) Clear to translucent, zero precipitation Loss on Drying (LOD) ≤6.0% (USP <731> / EP 2.2.32)
Bulk Density Range 0.35 – 0.55 g/mL Tapped Density Range 0.55 – 0.75 g/mL Heavy Metals Pb ≤1.0 ppm; As ≤1.0 ppm; Cd ≤0.1 ppm; Hg ≤0.1 ppm (Compliant with USP <233> / EP 2.4.20) Residuos de plaguicidas Complies with European Regulation (EC) No 396/2005 Standard Microbiological Security Total Plate Count ≤1,000 cfu/g; Yeast & Mold ≤100 cfu/g; Salmonella & E. coli: Absent per 10g ¿Busca un presupuesto?Póngase en contacto con nosotrosRequest a Custom QuoteQuality & Compliance
Global Food-Grade Compliance: Manufacturing infrastructure and food facility operations are audited and certified under BRCGS, IFS, ISO 9001, and ISO 22000 quality management standards to verify trace-level international supply chain compliance.
Dietary & Organic Status: Materials maintain documented Halal, Kosher, EU Organic, and USDA Organic status, qualifying the ingredient for immediate cross-border commercial customs clearance and global market accessibility.
Elemental Contaminant Controls: Batch testing via ICP-MS verifies individual heavy metal limits adhere to pharmacopeial parameters (Pb ≤1.0 ppm, As ≤1.0 ppm, Cd ≤0.1 ppm, Hg ≤0.1 ppm), with pesticide residues compliant with European Commission regulations.
Microencapsulation Matrix Integrity: Analytical data packets confirm residual carriers and matrix materials conform to international food additive criteria. The spray-drying verification sequence ensures uniform structural protection of the active core without trace cross-contamination from unapproved processing aids.
Liquid-Optimization Microbial Security: Standard quality control protocols enforce strict biological risk limits tailored for hydration formulations, verifying Total Plate Count ≤1,000 cfu/g and Yeast & Mold ≤100 cfu/g, with documented absence of Salmonella and E. coli per 10g to accelerate internal QA/QC vendor qualification.
Key Advantages
Instant Cold-Water Dispersibility: Formulated to resolve the processing bottlenecks of hydrophobic botanical crystals, the microencapsulated matrix achieves rapid, uniform dispersion in cold liquid media without clumping, high-shear mixing, or industrial heating protocols.
Homogeneous Dispersed Visual Stability: Engineered to maintain a stable, clear-to-translucent (opalescent) appearance without sedimentation across wide industrial pH ranges. The hydrophilic carrier network prevents active agglomeration, ensuring functional beverages, liquid wellness shots, and syrups preserve clean sensory aesthetics during commercial distribution.
Organoleptic Bitterness Masking: Utilizing a cross-linked protective polymer shell, the physical microencapsulation matrix effectively coats the active core to mask the natural astringency and sharp bitterness characteristic of plant polyphenols. This technical configuration eliminates the requirement for heavy synthetic flavor-masking additives in clean-label or sugar-free formulations.
Thermal & Processing Resilience: Exhibiting documented physical and chemical stability during standard pasteurization, UHT sterilization, and high-temperature commercial lines, the protected active core resists thermal degradation and discoloration, maintaining verified batch-to-batch dosing precision and ingredient uniformity.
Applications
Ready-to-Drink (RTD) Functional Beverages: Standardized as an advanced cold-water dispersible aglycone constituent for functional sports waters, ready-to-drink tea bases, and carbonated recovery drinks. The hydrophilic carrier matrix ensures a stable, clear-to-translucent (opalescent) appearance without material separation or active sediment during commercial distribution.
Instant Powder Drink Mixes & Stick Packs: Tailored specifically for high-speed automated packaging lines processing single-serve powder stick packs, pre-workout hydration mixes, and dry-blended meal replacements. The standardized 100% through 80 mesh granulometry enables homogeneous dry blending into nutritional food matrices without altered physical stratification or gritty texture.
Nutraceutical Confectionery & Gummies: Approved for modern fortification lines processing active health gummies, compressed chewable tablets, and fortified lozenges. The cross-linked microencapsulation shell prevents active ingredient thermal degradation during high-temperature cooking and matrix depositing utilizing gelatin or pectin bases.
Liquid Dietary Supplements & Syrups: Engineered for clean-label liquid vitamin complexes and localized botanical drop formulations that chemically accommodate an opalescent fluid baseline. The physical microencapsulation protection controls continuous material uniform suspension, eliminating batch-to-batch active ingredient heavy precipitation during extended shelf-life storage.

Technical FAQ
Q1: What is the carrier composition of this 20% water-soluble quercetin, and does it require novel food status authorization?
A: This ingredient is a physical matrix where high-purity quercetin is embedded within a food-grade hydrophilic maltodextrin or arabic gum carrier network via spray-drying microencapsulation. Because the native chemical structure of the bioflavonoid aglycone remains unaltered without enzymatic modification or chemical synthesis, the constituent utilizing approved food additives conforms to standard global regulatory frameworks for functional food ingredients.
Q2: How does this microencapsulated quercetin powder 20% perform under industrial heat treatment like UHT processing or pasteurization?
A: The cross-linked polymer outer shell provides technical shielding for the active core. Standardized testing confirms the material maintains a verified active retention rate during standard UHT processing (135°C–140°C for 4 seconds) and pasteurization (85°C for 30 minutes). The dissolved matrix yields a stable, clear-to-translucent (opalescent) appearance with zero thermal discoloration or chemical degradation across a factory pH range of 3.0 to 7.2.
Q3: Is there a maximum saturation limit for this microencapsulated quercetin powder in liquid formulations to prevent long-term active sedimentation?
A: The ingredient exhibits a practical operational saturation ceiling of approximately 15–20 g/L in ambient aqueous media. For long-term physical stability in commercial functional beverages and ready-to-drink (RTD) liquid supplements, an industrial standard dosing concentration of 100mg to 250mg per 250mL bottle is advised. Maintaining this formulation profile prevents material particle agglomeration, preserving product uniformity over a standard 24-month shelf life.
Why Partner with Green Spring Technology?
26-Year Phytochemical Expertise: Operating as an industrial botanical extraction manufacturer since 2000, Green Spring Technology specializes in batch-stable bioflavonoid isolation and ingredient standardization for global food, beverage, and nutraceutical industries.
International Regulatory Compliance: Manufacturing facilities and processing operations conform to verified BRCGS, IFS, ISO 9001, and ISO 22000 quality management standards to support cross-border commercial customs clearance.
Traceable QA/QC Supply Chain: Utilizing an in-house testing laboratory equipped with analytical HPLC, GC-MS, and ICP-MS instrumentation, the infrastructure enables comprehensive seed-to-extract traceability, verified batch uniformity, and documented transparency from raw materials to final bulk delivery.
-
Download Data Sheet: COA, TDS, MSDS Please fill in the form below to receive the full technical documents via email.